Conveyors & Handling
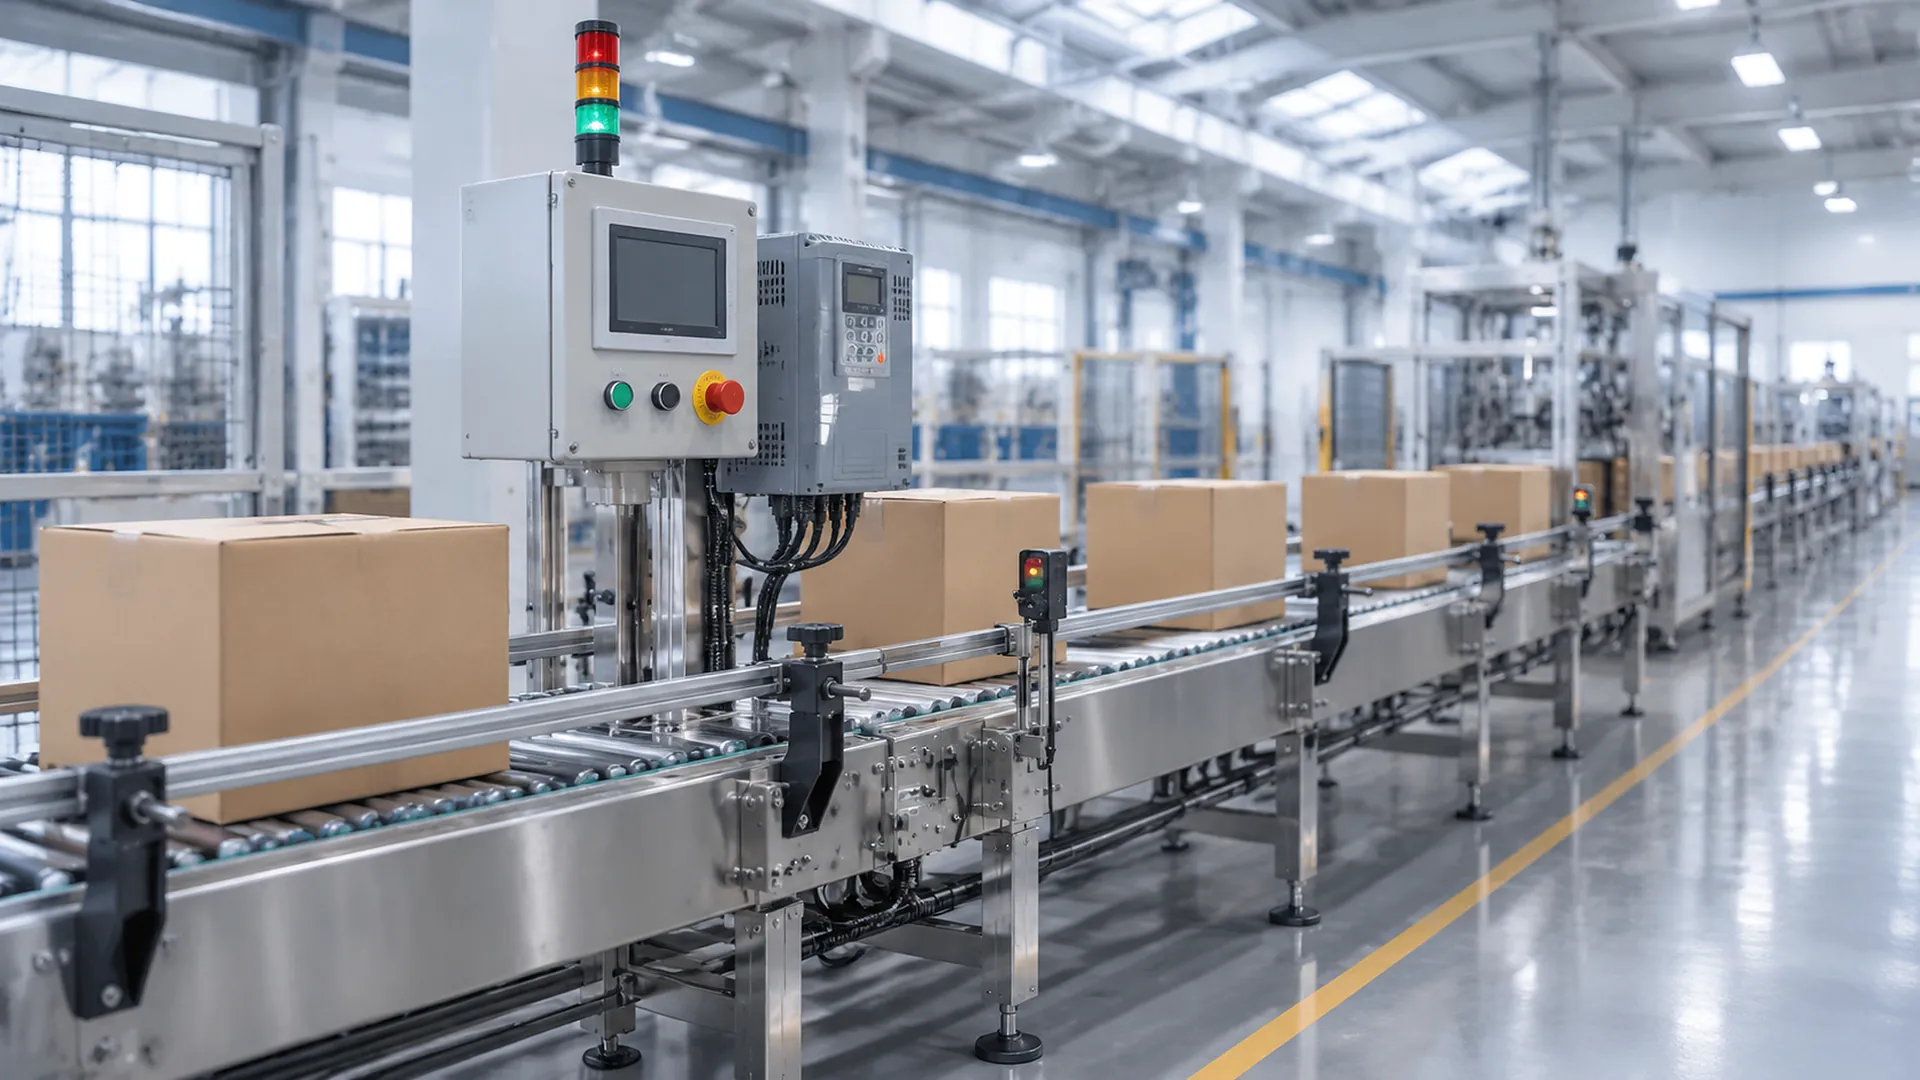
Drives for conveyors and handling lines.
A conveyor is a constant-torque load that starts loaded, so the G rating and usually one frame up is the cheaper decision. S-curve acceleration and DC braking without a brake resistor are what keep the product on the belt.
This duty at a glance
A frame number is only issued against the duty point: send the curve, the cycle or the belt data and the rating comes back confirmed, not estimated.
Platforms used for this duty
What this duty actually asks of the drive
The mechanical problem is inertia. A loaded belt has to come up to speed without snatching, and it has to stop without the load sliding forward. Both are solved in the ramp: an S-curve profile removes the step at the start and the jerk at the stop, and DC braking holds the motor after the ramp instead of letting it coast.
The electrical problem is that the start is loaded. Unlike a fan or a centrifugal pump, a conveyor needs close to full torque from zero speed, so the frame is chosen on the G rating and one frame up when the ramp is short or the belt is long and heavy.
On a multi-zone line the drives also have to know about each other: a downstream zone that stops must not pile product into the zone behind it. That is a speed-reference and interlock exercise, and it is the part of a conveyor project that the integrator wants confirmed before the order.
How the frame is chosen
| Duty condition | Frame rule | What gets set |
|---|---|---|
| Loaded horizontal belt | G rating, one frame up on short ramps | S-curve acceleration, DC braking enabled |
| Incline or decline section | G rating, one frame up | Braking torque confirmed against the slope load |
| Multi-zone line with accumulation | G rating per zone | Speed reference and interlock between zones configured |
| Long cable run to a remote zone | Frame unchanged | Carrier reduced to 4 kHz or below |
Frame numbers are issued against the duty point, not against the motor nameplate. Send the load profile — curve, head, cycle or belt data — and the rating is confirmed on it.
Where this platform stops
A page that claims to cover every case is worth less than one that says where the catalogue ends. These are the limits that decide whether the answer is a standard frame, a cabinet build, or a different platform entirely.
Questions that come before a purchase order
Do I need a brake resistor to stop a conveyor?
For a horizontal belt that stops under its own friction, no: DC braking holds the motor after the ramp without an external resistor option. A decline where the load overhauls the motor does need braking hardware, and that is quoted with the frame.
Why one frame up instead of the frame at motor rating?
Because the start is loaded. The G rating is the constant-torque rating, and a conveyor draws close to full torque from zero speed with a short ramp. Sizing on the motor nameplate works on a fan and under-sizes a belt.
Can the drive link to the line PLC?
RS-485 Modbus RTU is standard on G600, and it is what a line PLC uses for the speed reference, the run command and the fault word. The register map is what the integrator commissions against.
What is the minimum order for a line of several zones?
Minimum order is 1 piece per frame; private label and custom builds start at 100 pieces. A multi-zone line is quoted as a frame list with the parameter files, at the published 10-day lead time for 1–5,000 pieces.
Other duty profiles
Next step
Send the duty point. Get a frame number back.
Power, voltage, load type and the number of units is enough to quote. Anything short of that gets a question back the same working day.
- ≤ 3 h
- Reply on a working day
- 1 pc
- Minimum order
- 10 days
- Lead time to dispatch
- CE LVD/EMC
- ISO 9001 plant